Ceramic Dry Pressing for Defined Part Geometry
Connect ceramic dry pressing to your drawing, mating surfaces, service conditions, and acceptance requirements before requesting a quotation.
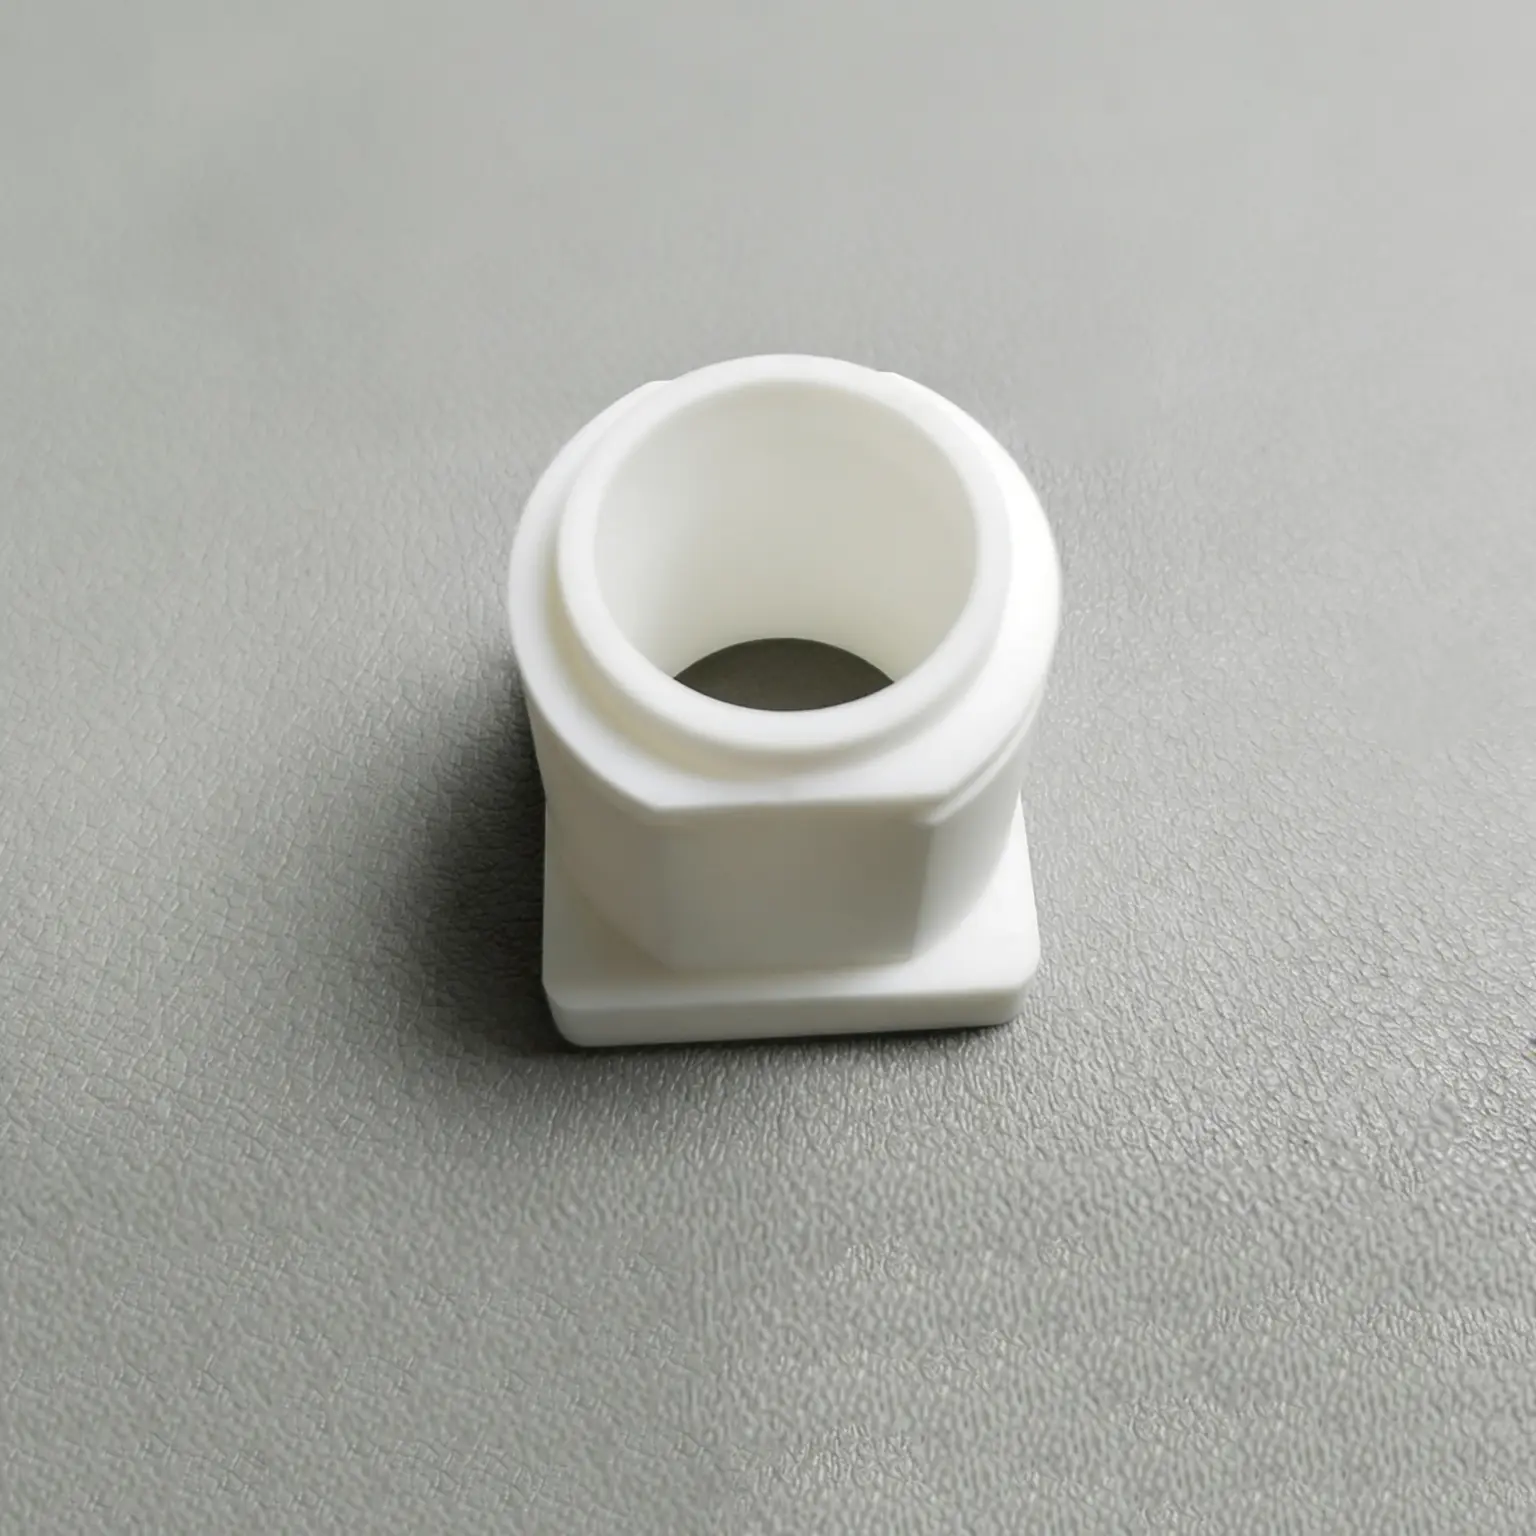
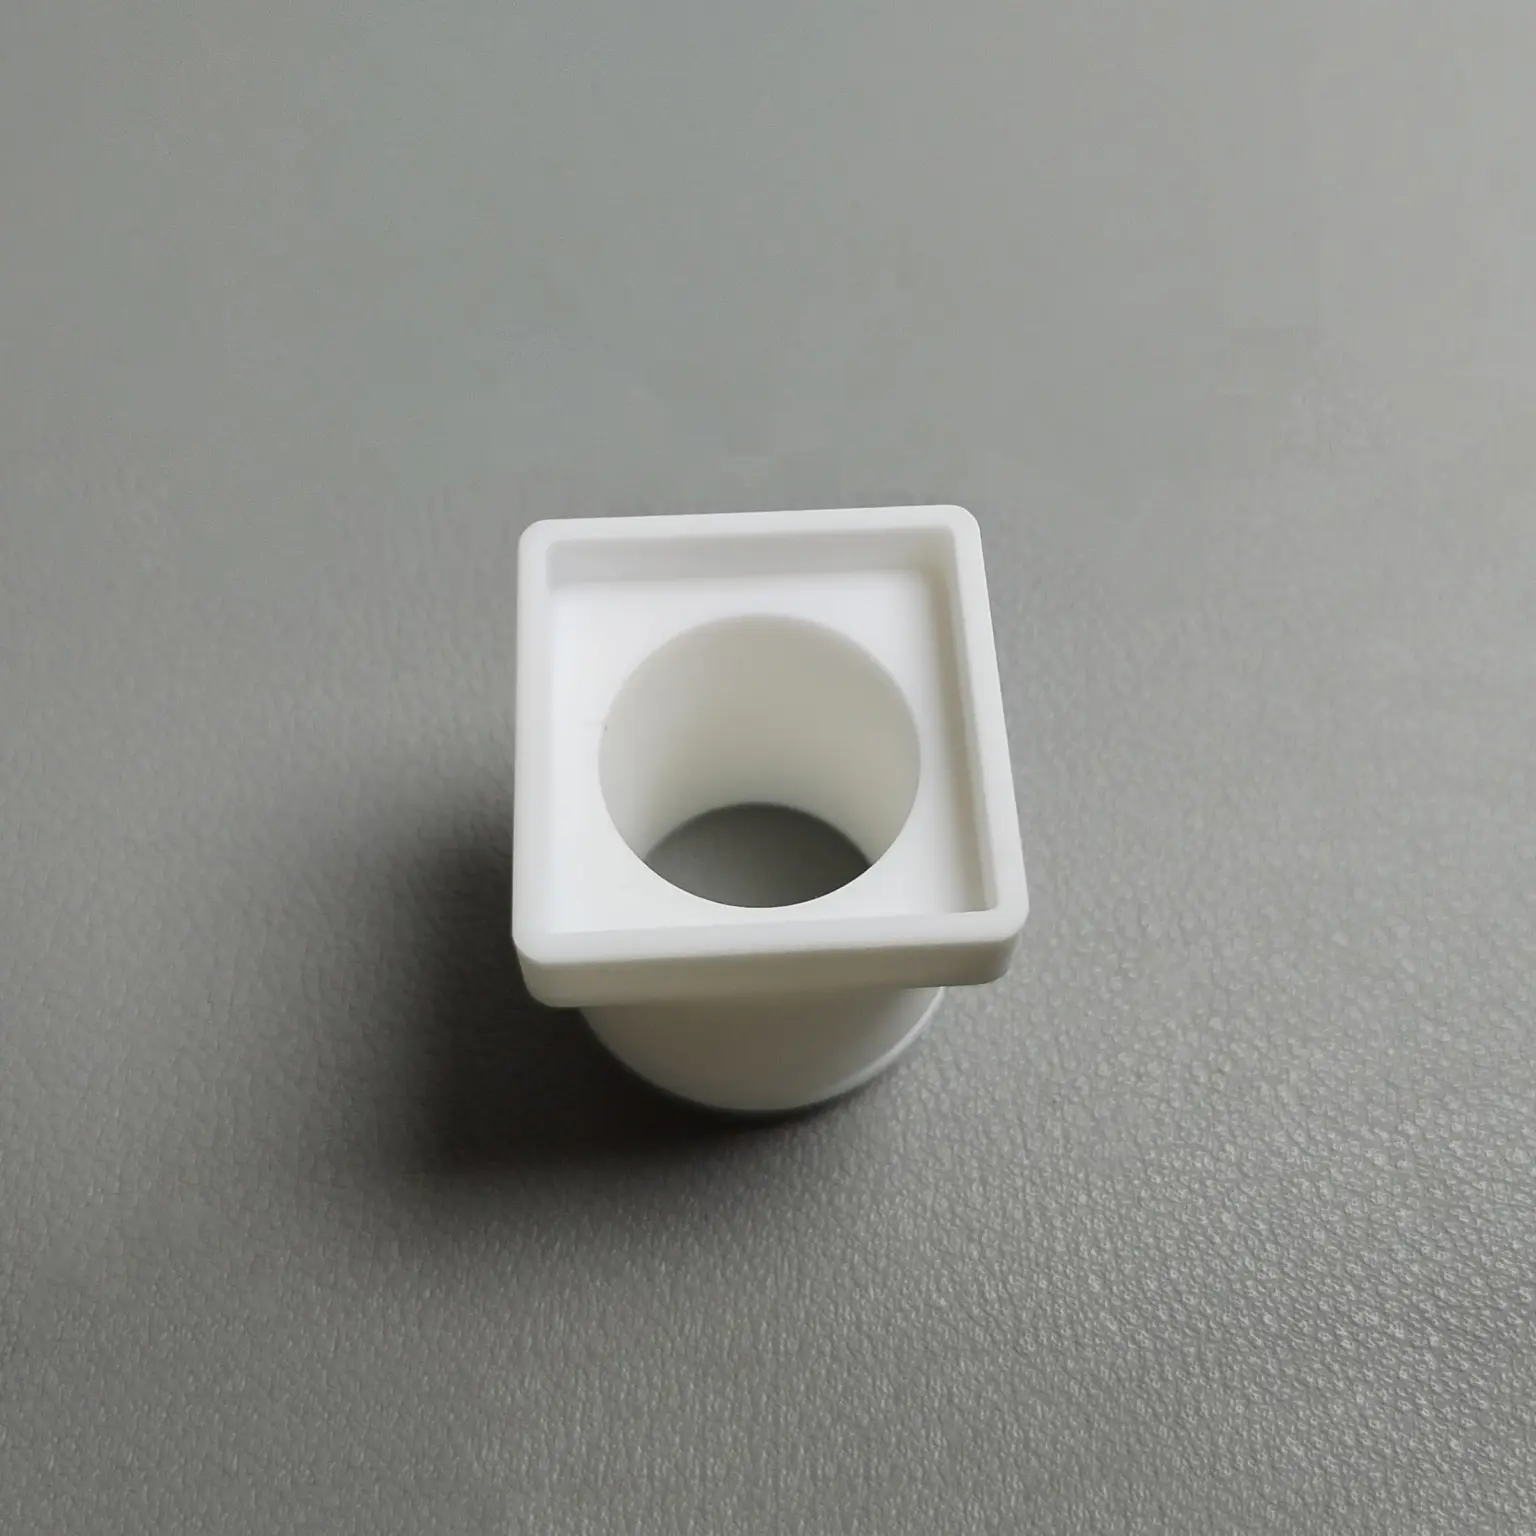
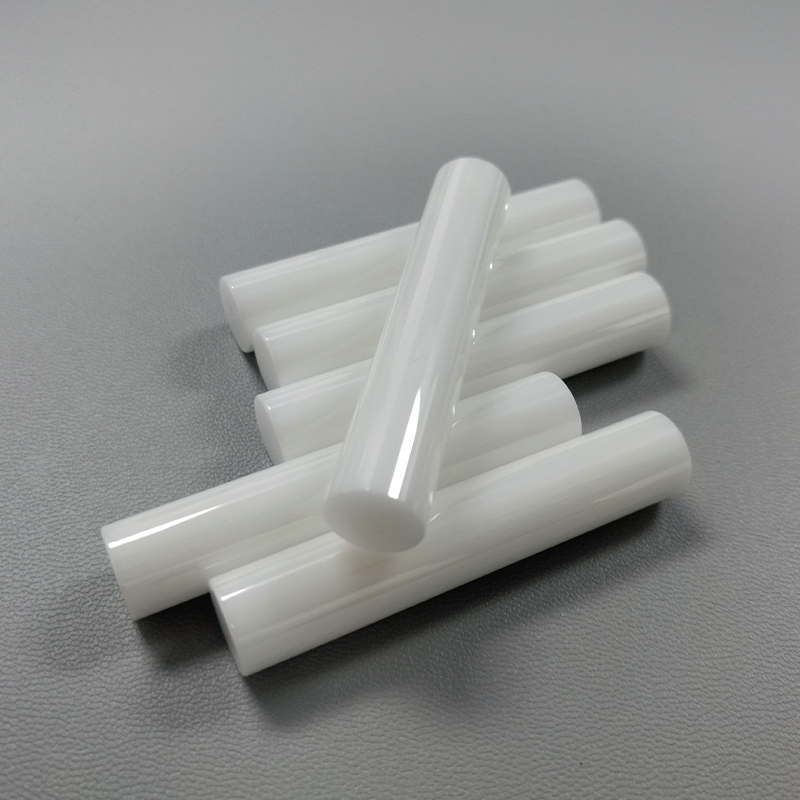
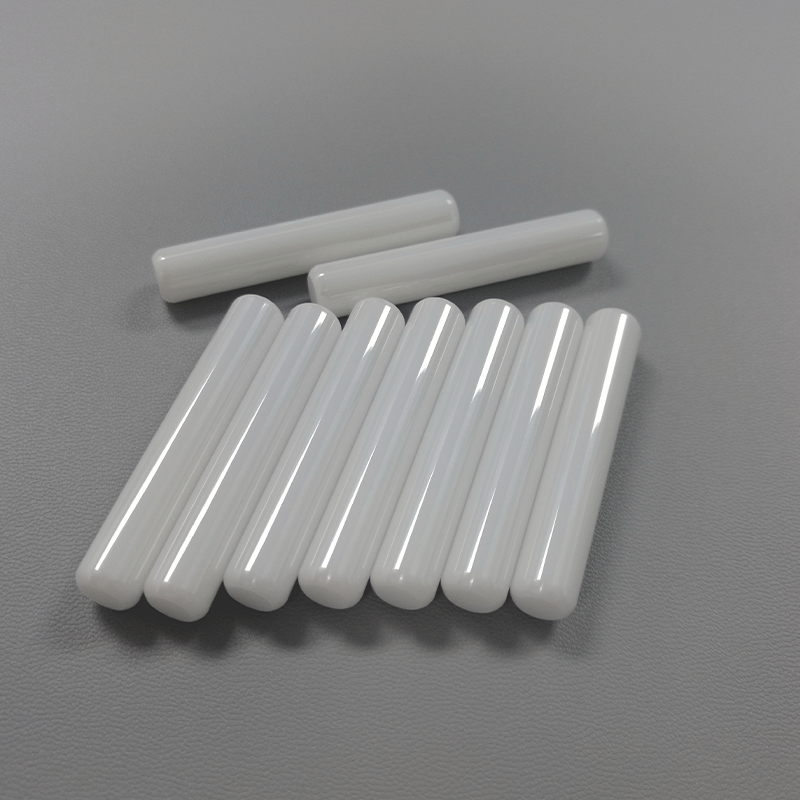
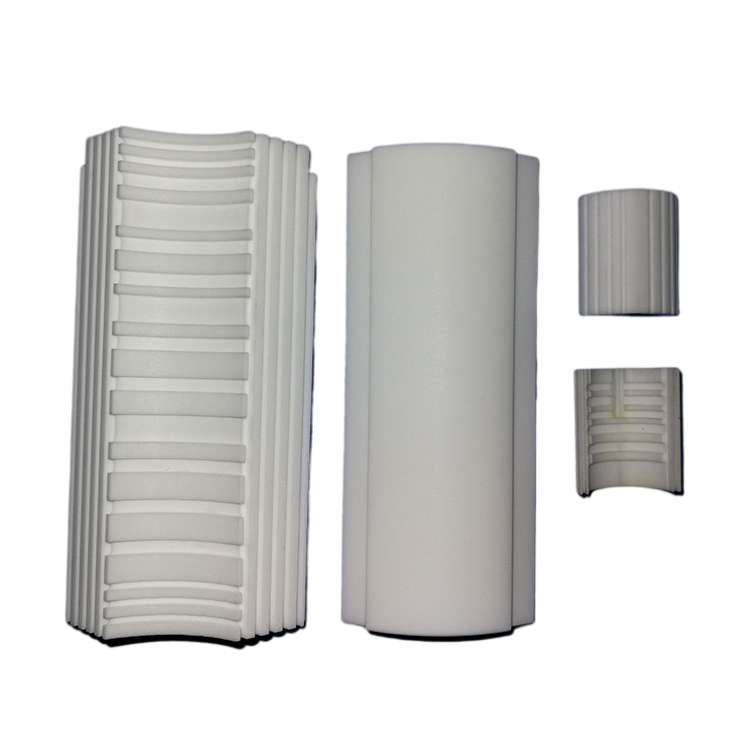
Featured Industrial Ceramic Parts for Dry Pressing

What to Define Before Ceramic Dry Pressing
Evaluate the drawing, material, geometry and acceptance details that shape a productive ceramic dry pressing discussion.
Current Drawing Revision
Provide the current drawing revision and identify controlled dimensions, interfaces and notes so the quotation discussion begins from the part requirement rather than a general illustration.
Grade Matches Service Conditions
Name the ceramic grade when known, then describe temperature, electrical, wear, chemical or mechanical conditions that may affect material selection for the individual component.
Die-Led Geometry Review
Review wall relationships, cross-sections, features and parting considerations early. Ceramic dry pressing uses a die and punch arrangement, so geometry should be assessed with the forming route.
Functional Surfaces Identified
Mark surfaces that mate, seal, locate or support another part. Their function helps focus discussion on dimensions, finish expectations and any post-forming processing requirements.
Quantity Supports Planning
Share anticipated order quantity and whether the need is a prototype, replacement or recurring program. This helps frame process-route and tooling discussions without implying a commitment.
Inspection Evidence Defined
State the acceptance criteria, inspection records and documentation needed for approval. Clarifying evidence requirements alongside the drawing reduces uncertainty before an order is agreed.
Explore Related Ceramic Options
Compare forming routes, material families, applications and component references before defining the next step for your drawing-led inquiry.
Ceramic Manufacturing Capabilities
Review ceramic manufacturing capabilities alongside your component requirements. Forming route, geometry, machining allowance, mating surfaces and inspection needs should be considered together before a quotation discussion begins.
Explore Capabilities
Ceramic Solutions by Industry
Explore advanced ceramics applications by operating environment and component function. Service temperature, wear, electrical behavior, chemical exposure and assembly constraints help identify which questions a project team should resolve first.
Explore Industries
Advanced Ceramic Materials
Compare advanced ceramic materials across oxide, nitride, carbide and specialty families. General material information is a starting point; grade selection, geometry and project-specific acceptance requirements require confirmation.
Explore Materials
Technical Ceramic Products
Browse technical ceramic products by familiar component forms, including tubes, rods, rings and substrates. Use the relevant product page to frame an inquiry around the drawing revision, dimensions and intended service conditions.
Explore Products
Technical Ceramic Resources
Use this technical ceramics guide to prepare a clearer inquiry. Identify the part function, material designation if known, critical dimensions, mating surfaces, quantity, operating conditions and required documentation.
Explore ResourcesPorcecore’s Ceramic Dry Pressing Approach
Porcecore was founded by Andy Yuan to make technical ceramic sourcing more understandable for industrial buyers, equipment builders, and project teams. For custom ceramic components and ceramic dry pressing inquiries, we begin with the component and its intended job, helping turn an initial material or replacement-part question into a clearer technical discussion.
Our scope covers technical ceramic materials and familiar component forms, including tubes, rods, rings, and substrates. We do not treat a material name or product illustration as a final specification. Grade, geometry, mating surfaces, service conditions, and inspection expectations must be considered for the individual project.
What distinguishes Porcecore is a drawing-led, application-first approach. Send the current drawing revision, known material designation, quantity, operating conditions, and acceptance criteria so the quotation conversation has a concrete basis. Email info@zlrsmaterials.com or message WhatsApp at +86 130 6482 5920 to discuss your requirement.
Key Ceramic Dry Pressing Controls
Powder Condition First
Ceramic dry pressing begins with powder condition suited to the intended component. Discuss material family, granulation, binder approach, flow behavior, and moisture expectations alongside the part geometry, rather than treating the powder as a separate purchasing detail.
- Material designation or preferred ceramic family
- Powder flow and fill considerations
- Binder and moisture requirements to confirm
- Grade-specific properties subject to project review

Die and Punch Geometry
The die cavity and punch faces define the compact before firing, so geometry deserves drawing-level attention. Identify critical profiles, wall transitions, holes, edges, and surfaces that interface with other parts; these details help frame a practical ceramic dry pressing discussion.
- Current drawing revision and nominal dimensions
- Critical holes, recesses, and profile features
- Mating surfaces and assembly-driving dimensions
- Tolerance and surface expectations to review

Compaction Consistency
A useful inquiry distinguishes dimensions that matter from dimensions that merely describe the part. For ceramic dry pressing, section thickness, feature distribution, density expectations, and acceptance criteria should be reviewed together to clarify which controls are essential for the application.
- Sections that may need density review
- Thickness changes across the component
- Performance conditions affecting acceptance
- Inspection and documentation needs

Green-Body Handling
The formed green body is an intermediate stage, not the finished component. Clarify how the part will be handled, machined if applicable, fired, inspected, and delivered, with particular attention to fragile features and any requirements that must be verified after sintering.
- Fragile features and handling considerations
- Post-forming operations to discuss
- Final inspection points and records
- Quantity, delivery, and packaging requirements

Ceramic Dry Pressing vs. Cold Isostatic Pressing
Compare drawing requirements, geometry, and inspection priorities before selecting a forming route for your ceramic part.
← Swipe left or right to view →
Ceramic Dry Pressing Production Flow
A drawing-led sequence for aligning component geometry, powder behavior, die conditions and inspection expectations before next-stage processing.
Review Part Requirements
Confirm drawing revision, material designation, critical dimensions, mating surfaces, service conditions, quantity and acceptance criteria to establish a clear ceramic dry pressing inquiry basis.
Prepare Granulated Powder
Assess powder grade, particle distribution, flowability, moisture and binder requirements for the selected component geometry and intended compaction approach.
Fill the Die
Introduce prepared powder into the die cavity with attention to fill consistency, cavity geometry and features that can influence local density.
Compact the Powder
Apply the defined pressing sequence to form a green body, considering pressing direction, tool configuration and the part features needing controlled geometry.
Eject and Inspect
Remove the green body carefully, then review visible condition, key dimensions and handling integrity against the project’s agreed inspection expectations.
Define Next Processing
Align the next-stage route, including firing and any required finishing or documentation, with the individual part requirement before production commitments are confirmed.
How to Start a Ceramic Dry Pressing Inquiry
Share the details that turn an initial ceramic component request into a focused quotation discussion.
Send the Current Drawing
Provide the latest drawing revision and identify the dimensions, features, and mating surfaces that control assembly, fit, or functional performance.
Define Material and Quantity
State the material designation if known, required component quantity, and whether the request concerns a new design, replacement part, or ongoing demand.
Describe Service Conditions
Explain the operating environment, including temperature, media, loading, electrical requirements, and other conditions that may influence material and geometry discussions.
Clarify Acceptance Requirements
Identify critical tolerances, inspection expectations, documentation needs, surface requirements, and any criteria your team will use to evaluate the proposed ceramic dry pressing solution.
What to Confirm Before a Ceramic Dry Pressing Project
Verified customer case pending publication. This space will document a ceramic dry pressing outcome with the approved drawing revision, inspection result, quantity, and customer-authorized wording before it is presented as a testimonial.
Verified customer case pending publication. A finalized testimonial will identify the component requirement, documented fit, durability, delivery, or inspection outcome, plus the customer-approved number and attribution where permission is available.
Verified customer case pending publication. Porcecore will add only approved evidence tied to a ceramic dry pressing project, including the relevant part geometry, acceptance criteria, and measurable result, rather than a generalized performance claim.
Ceramic Dry Pressing FAQ
Clarify the drawing, material, tooling and acceptance inputs before requesting a project-specific quotation.
Which component geometries are suitable for ceramic dry pressing?
How should I select a material grade for ceramic dry pressing?
What tolerances can a ceramic dry pressing part achieve?
Does ceramic dry pressing require dedicated tooling?
Can secondary machining be specified after pressing and firing?
How do quantity, MOQ, lead time, and sampling affect a quotation?
What inspection evidence should I request for a pressed ceramic component?
What files and application details should I send for a ceramic dry pressing inquiry?
Complete Buyer’s Guide to Ceramic Dry Pressing
Use this decision framework to assess process fit, powder and tooling requirements, supplier capabilities, quality controls, and total cost—while avoiding specification gaps, unrealistic tolerances, and sourcing mistakes that can disrupt production.
1. What Is Ceramic Dry Pressing?
Ceramic dry pressing is axial compaction of prepared granulated powder in a rigid die-and-punch arrangement to produce an unfired green body. The powder fills the die, punches compact it, and the part is ejected before sintering develops its final ceramic structure.
For procurement, the process is commonly considered for repeatable parts whose geometry, critical faces, tolerances, and production volume justify dedicated tooling. Final dimensions must account for sintering shrinkage and grade-specific behavior; moisture targets and process settings require confirmation for the individual material and part.
Reference: https://www.osti.gov/biblio/247990
2. Evolution of ceramic dry pressing
1996 technical-ceramics guidance already described dry pressing as axial compaction of granulated powder in die-and-punch tooling, with uniform green density and defect-free compacts as core goals (https://www.osti.gov/biblio/247990). Conventional single-action pressing exposed the effects of friction, powder fill, and tool alignment on density variation.
Two-punch, multi-action, rotary, and automated systems expanded control over fill, compaction, and ejection. Consistent granule size distribution, flowability, binder content, and moisture became essential because the press can only repeat the powder condition it receives.
Today, buyers commonly expect controlled tooling revisions, recorded process settings, lot identification, and inspection records alongside scalable output. For ceramic dry pressing, a repeatable part therefore depends on linking the drawing, powder specification, press setup, and acceptance criteria—not on a material name alone.
3. Types of ceramic dry pressing
Five press routes differ mainly in punch motion and powder travel. In ceramic dry pressing, shape, thickness, density uniformity, tolerance, and volume determine the practical route.
1996 technical-ceramics literature lists rotary, multiple-punch, and multiple-action configurations: https://www.osti.gov/biblio/247990
| Route | Pressure Direction | Suitable Scenario | Buyer Question |
|---|---|---|---|
| Single-action | One axial punch | Thin, simple forms | Is one-sided density acceptable? |
| Double-action | Opposing axial punches | Thicker sections | Is density balance needed? |
| Multi-level | Several punches | Stepped geometry | Can features form in one press? |
| Rotary | Repeated axial stations | High-volume standard parts | Does volume justify dedicated tooling? |
| Isostatic | All-around pressure | Uniform-density need | Is a non-die route better? |
Axial Press Choices
Single-action compacts from one side; double-action uses opposing punches. Double-action can reduce through-thickness density variation, but tooling and setup are more involved.
Complex And High Volume
Multi-level or multi-punch tooling forms steps or multiple features in one stroke. Rotary pressing favors repeatable, high-volume simple parts, while tool wear and geometry limits require review.
Isostatic Alternative
Isostatic pressing applies pressure around the compact rather than only axially. Ask whether improved density uniformity justifies a different route for the required shape and tolerance.
4. Ceramic dry pressing materials and powders
Material selection starts with service: wear, insulation, temperature, strength, and electrical behavior. Ceramic dry pressing also depends on granules that fill the die consistently and shrink predictably during sintering.
| Material | Key Property | Typical Requirement |
|---|---|---|
| Alumina | Wear, insulation | Seals, insulators |
| Zirconia | Strength | Tough components |
| Silicon carbide | Thermal resistance | Hot-duty parts |
| Steatite | Electrical insulation | Electrical fittings |
| Ferrite | Magnetic behavior | Magnetic cores |
Match Material To Duty
Alumina suits wear and insulation; zirconia favors strength; silicon carbide supports thermal duty. Ferrite and dielectric formulations require electrical properties to be specified by grade.
Control The Powder System
Granule size distribution and flowability govern die fill and green-density uniformity. Binder and lubricant must support compaction and release; free moisture, often below 3% for technical dry pressing, should be controlled with the sintering schedule. https://www.osti.gov/biblio/247990
5. Ceramic dry pressing design options
Before tooling release, ceramic dry pressing design decisions should be tied to the part’s mating functions. Porcecore recommends supplying the current drawing revision, material designation, quantity, service conditions, inspection requirements, and assembly-critical surfaces.
Formed Versus Machined Features
External profiles, through-holes, simple steps, and grooves may be formed in the die when they align with the pressing direction. Deep side details, cross-holes, threads, tight fits, and precision surfaces commonly require secondary machining after firing.
Wall-thickness transitions and abrupt section changes can disrupt powder filling and density uniformity. Each added punch, core, or complex contour can increase tooling complexity, yield risk, and cost.
Specify Functional Requirements
Drawing callouts should identify datum surfaces, dimensions that control assembly, tolerances, surface-finish needs, markings, and permitted material or color alternatives. Grade-specific properties and final dimensions require confirmation for the individual project.
Secondary machining should be reserved for features that cannot be reliably pressed or whose tolerances are functional. Buyers should distinguish cosmetic preferences from acceptance-critical requirements before quotation and tool design.
6. Quality factors in dry-pressed parts
Uniform green density is the first quality control point in ceramic dry pressing; density gradients can become uneven shrinkage, lamination, or cracks after firing. Acceptance criteria should tie drawing-critical dimensions and functional surfaces to the finished, sintered part.
Compaction Inputs
Die wear, powder fill uniformity, pressing force, speed, and dwell affect compact density. Review die-maintenance status and press-setting records for each lot.
Finished-Part Checks
Sintering control determines final size, flatness, porosity, surface defects, and property variation. Specify measurement methods, sampling plan, dimensional tolerances, allowable chips or cracks, and any required mechanical or electrical tests.
Lot Consistency
Lot records should link powder batch, green-part checks, firing cycle, inspection results, and nonconformance disposition. Confirm which records, test values, and certificates are required before quotation and production approval.
7. Choosing a ceramic dry pressing manufacturer
A ceramic dry pressing supplier should be evaluated against the drawing, not a catalog claim. Request evidence early so capacity statements can be separated from records for the proposed part.
Review The Drawing
One engineering review should identify critical dimensions, mating surfaces, datum scheme, material, quantity, and service conditions.
Two open questions are enough to delay quotation: unclear tolerances or undefined acceptance criteria.
Verify Process Evidence
One RFQ package should request comparable material experience, powder controls, press range, tooling-maintenance practice, inspection plan, and secondary-operation route.
Two sample-approval records matter most: dimensional results and the applicable material or process documentation.
Control Production Transfer
One prototype approval should define the released drawing revision, inspection method, documentation, lead-time assumptions, and change-notification path.
Two production questions remain: how tooling changes are approved and how lot-to-lot inspection records are retained.
8. Common ceramic dry pressing sourcing mistakes
Ceramic dry pressing purchase risk often begins before the quotation. Convert each assumption into a drawing note, inspection requirement, or supplier question before releasing the purchase order.
Shrinkage And Geometry
Final dimensions alone omit firing shrinkage and can misstate tool dimensions. Correct it: identify controlled dimensions after firing and ask: What shrinkage allowance and tolerance basis will govern this shape?
Density In Thick Sections
Thick or stepped sections can compact differently across the part. Correct it: request a manufacturability review and ask: Which locations need density-risk review or sectioning?
Material And Tooling
A material family name does not define grade, finish, or service suitability. Correct it: specify the application and ask: Which grade and tooling timeline fit this drawing?
Samples, Tests, And Pricing
Prototype price and sample approval do not establish production acceptance. Correct it: define test methods, lot sampling, and inspection criteria; ask: What tests, acceptance limits, and production-price assumptions apply?
9. From drawing to production launch
A component program should not enter tooling until application, interfaces, and acceptance evidence are frozen. For ceramic dry pressing, each gate assigns an owner and a releasable record.
Define The Requirement
Gate 1 starts with the current drawing revision, mating surfaces, service conditions, annual volume, and required documents. Engineering owns function; procurement owns forecast.
Gate 2 records manufacturability questions, risk features, and material designation before quotation.
Release Tooling
Gate 3 aligns tolerances with the forming and finishing route, then defines inspection criteria. Equipment builders identify assembly-critical dimensions; distributors preserve revision traceability.
Gate 4 releases tooling only after the drawing revision and approval criteria are confirmed.
Validate And Control
Gate 5 validates first articles against the agreed inspection record before routine production. Approve packaging, labeling, lot identification, and logistics instructions before shipment.
Gate 6 requires written review for drawing, material, tooling, inspection, packaging, or process changes.
10. Ceramic dry pressing pricing and cost
1 quote should separate one-time tooling from recurring piece cost; illustrative tiers below are not Porcecore prices.
2 comparisons should use total landed cost: freight, packaging, incoming inspection, scrap risk, and tooling amortized over the stated production volume. Confirm yield assumptions, revision control, documentation, and lead-time basis before selecting the lowest unit figure.
| Order quantity | Cost drivers | Typical lead-time effect |
|---|---|---|
| Prototype / low volume | Tooling dominates; complex geometry and tight tolerances raise machining | Tool design and approval add time |
| Pilot volume | Material grade, inspection plan, and yield assumptions become visible | Sampling and revisions can extend schedule |
| Production volume | Tooling amortization lowers unit cost; packaging and lot controls remain | Stable releases support predictable planning |
| Repeat order | Existing approved tooling may reduce setup exposure; verify wear and revision status | Capacity and inspection requirements govern timing |
Discuss Your Ceramic Dry Pressing Part
Email your drawing or operating conditions to clarify grade, geometry, acceptance criteria, and commercial requirements before the next project decision.